Vibrating Feeder Types Classification & Applications

A vibrating feeder is a critical, high-efficiency material handling machine designed to continuously and evenly convey bulk, granular, or powdered materials—such as ores, cement, grains, or chemical raw materials—from hoppers, silos, or bins to downstream processing equipment like crushers, screens, or mixers. Although the structure of the vibrating feeder is quite simple, it can vary greatly depending on different application scenarios. This article will take you through the types of vibrating feeders.


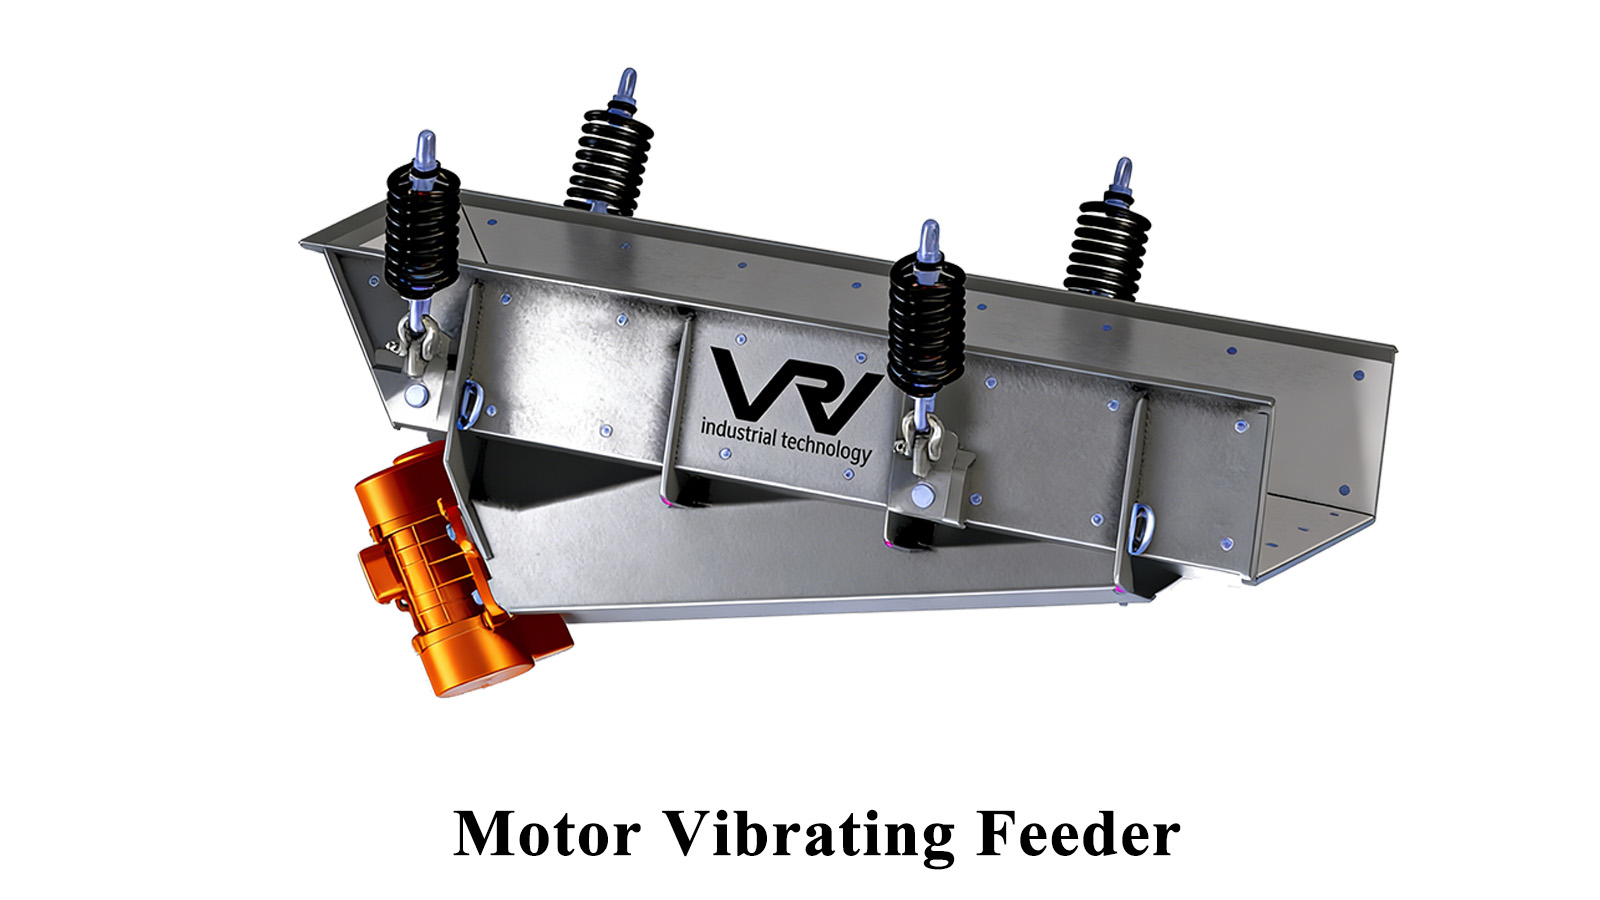
1. Motor Vibrating Feeder

The motor vibrating feeder is a high-efficiency industrial machine that uses vibration motors as the excitation source to convey bulk materials. It uniformly, continuously, and quantitatively feeds loose materials such as blocks, granules, and powders from storage bins or hoppers to downstream equipment like crushers, screens, or conveyors. Featuring a simple structure with core components including a trough, vibration motors, and shock-absorbing springs, it supports both suspended and seated installation for adaptability to complex working conditions. With adjustable vibration intensity and frequency via optional frequency conversion motors—it ensures stable and sensitive feeding while offering low maintenance costs and long service life. Widely applied in mining, metallurgy, coal, construction materials, chemical, and electric power industries, this reliable feeder enhances production line efficiency by preventing equipment blockages and stabilizing material flow.

Motor vibrating feeder for bulk materils

Features

1. Large feeding capacity

2. Simple structure & easy maintenance

3. Strong adaptability

4.Low energy consumption


2. Electromagnetic vibrating feeder

The electromagnetic vibrating feeder is an automated feeding machine that drives the tray or tube to vibrate reciprocally relying on an electromagnetic vibrator. It can uniformly, quantitatively and continuously convey bulk, granular or powdered materials from the storage bin to the receiving device. It features a simple structure, no need for lubrication, low energy consumption, and stepless adjustment of the feeding amount. It can achieve automatic control of the production process and is widely used in various industries such as mining, metallurgy, coal, chemical engineering, electric power, and grain.
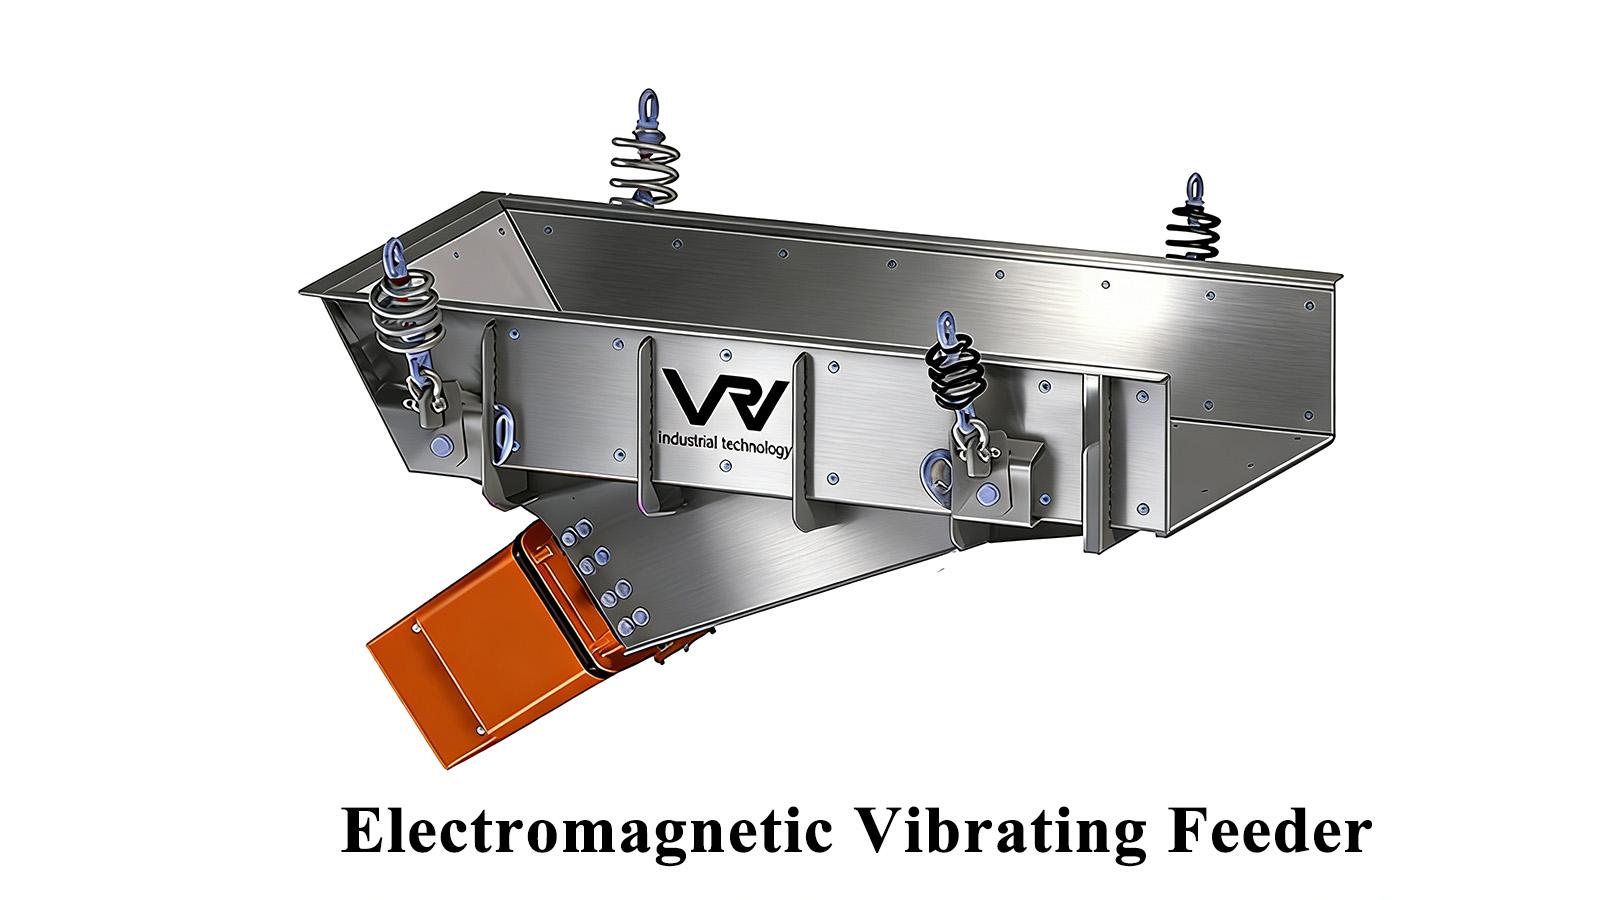

Electromagnetic vibrating feeder for bulk materials handling

Features

1. Precise feeding, stepless adjustment of output.

2. Energy-efficient, low power consumption.

3. Simple structure, easy installation and maintenance.

4. Gentle material handling, low breakage rate.

5. Low noise and dust, eco-friendly operation.

6. Fast start-stop response, suitable for automated systems.

7. No wearing parts, long service life.


3. Enclosed Vibrating Feeder

The biggest difference between the closed - type vibrating feeder and the open - type vibrating feeder lies in whether it has a closed trough structure. The closed - type vibrating feeder has a sealed trough that can completely enclose the trough and the material - conveying area. This can effectively prevent dust from flying during material transportation, reduce noise diffusion, and avoid external impurities from mixing into the materials. It is suitable for scenarios in mining, chemical industry, building materials, etc., where requirements for environmental cleanliness, material purity, or noise control are high. The closed - type vibrating feeder can use either a vibrating motor or an electromagnetic vibrator as the excitation source to provide power for the vibrating transportation of materials.
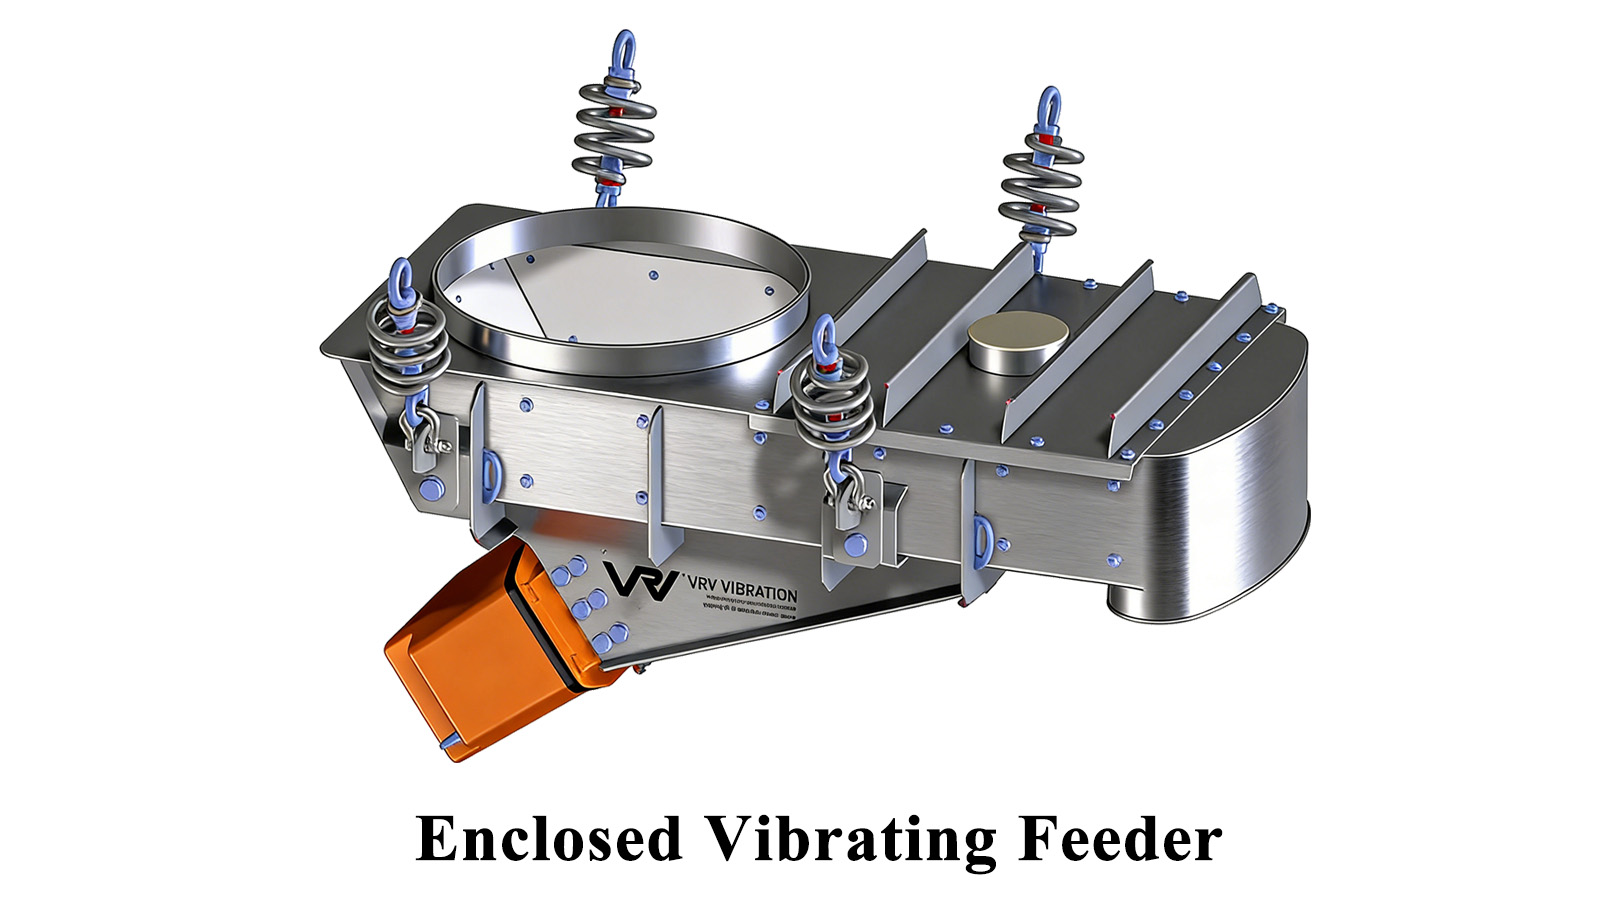
Closed - type Vibrating Feeder Dedicated for Dust Materials

Features

1. Sealed structure:Dust/leakage prevention

2. Stable feeding:Uniform & continuous delivery

3. Low energy consumption:High-efficiency, low power loss

4. Strong adaptability:Multi-material compatibility

5.Easy maintenance:Few wearing parts, easy repair


4. Compact Vibrating Feeder

The compact vibrating feeder is a material - conveying device with a small size and a compact layout. It is often equipped with a pedestal - type electromagnetic vibrator as the power source. Through vibration, it can uniformly and continuously feed materials such as granules and powders. It is suitable for production line scenarios with limited space. It has the characteristics of flexible installation, low energy consumption, and controllable feeding accuracy. It is widely used in the material pre - treatment or production transfer links of industries such as mining, chemical engineering, and food.Compact vibrating feeder for powder and granule materials
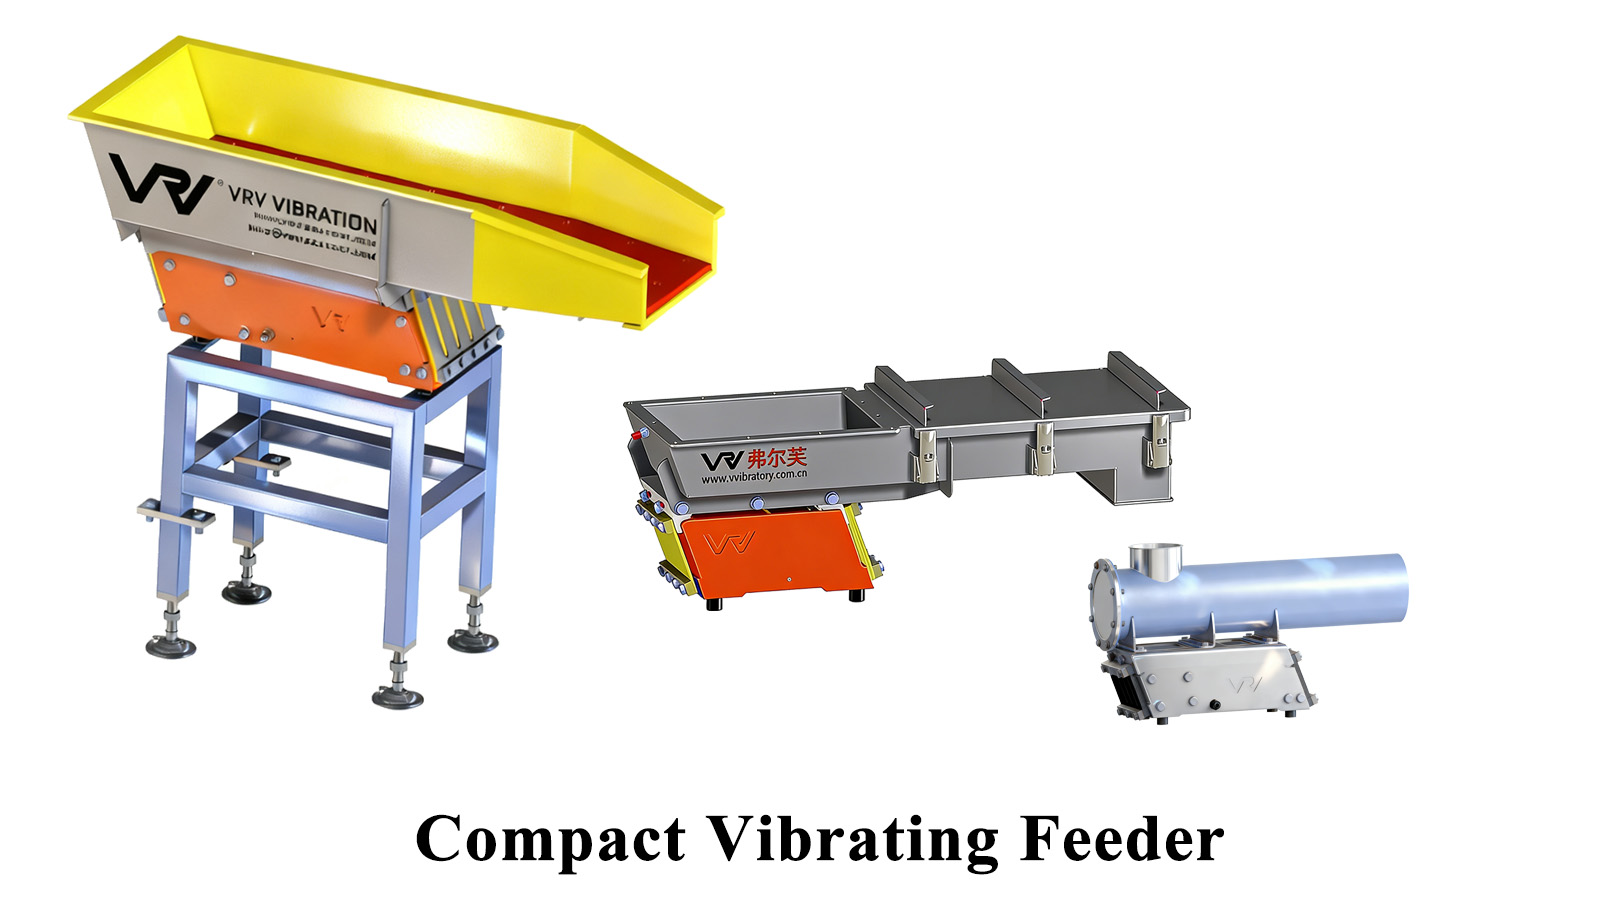
Features

1. Pedestal - mounted and no additional support is required.

2. Without rotating parts, it has a long lifespan and is maintenance - free.

3. With a compact structure, it takes up little space and is easy to operate.

4. Stable operation

5. High control accuracy and can start and stop without delay.

6. Low noise and low power consumption.


5. Vibrating Tube Conveyor

The Vibrating tube conveyor is a continuous feeding machine powered by vibration. Its core components include a sealed tubular trough, a vibrating motor (or exciter), an elastic support device, etc. The directional exciting force generated by the vibrating motor makes the powdered, granular or small - sized bulk materials in the tubular trough body perform continuous throwing or sliding movements, thus achieving smooth transportation and quantitative feeding from the feed inlet to the discharge outlet. It inherits the advantages of tubular equipment such as dust - tight sealing, a compact structure, and a small footprint. At the same time, due to its vibration - driven characteristics, material blockage is less likely to occur. Moreover, the feeding amount can be precisely controlled by adjusting the vibration frequency or amplitude. Compared with the screw - type tubular feeder, it has no internal rotating parts (such as screw blades), resulting in less wear and easier maintenance, making it more suitable for conveying materials that are prone to adhesion and blockage.
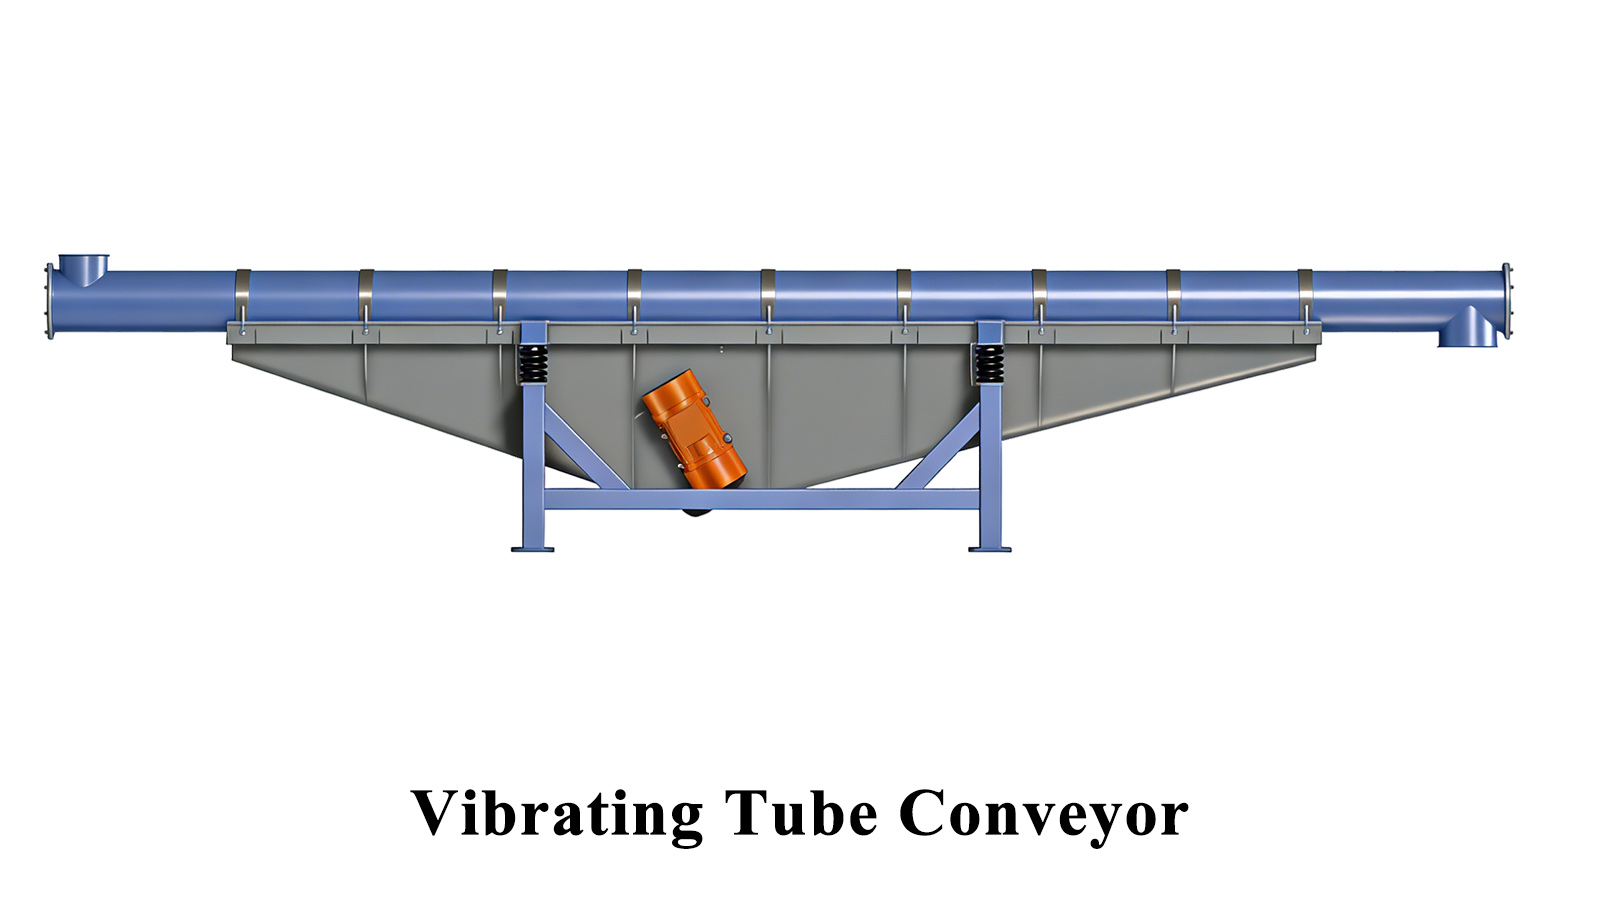
vibrating tube conveyor for bulk material conveying

Features

1. Continuous feeding: Provides continuous material feeding.

2. Sealed design: Keeps dust in and is dust - tight.

3. Compact structure: Occupies little space.

4. Vibration - driven: Reduces material blockage.

5. Precise control: Adjusts feeding amount via vibration.

6. Low - wear: No internal rotating parts, less wear.

7. Easy maintenance: Simple to maintain.


6. Long Vibrating Conveyor

Long Vibrating Conveyor is a high-efficiency long-distance conveying equipment designed for horizontal and slightly inclined transportation of powder, granular and bulk materials. Driven by vibration motors, it delivers stable and uniform material flow with low noise and easy maintenance. Equipped with a fully enclosed structure, it effectively avoids dust spillage and material contamination, and is widely applied in mining, building materials, chemical, food and other industries. We provide customized models with different lengths, materials (mild steel, stainless steel 304/316L) and conveying capacities to meet various working conditions.
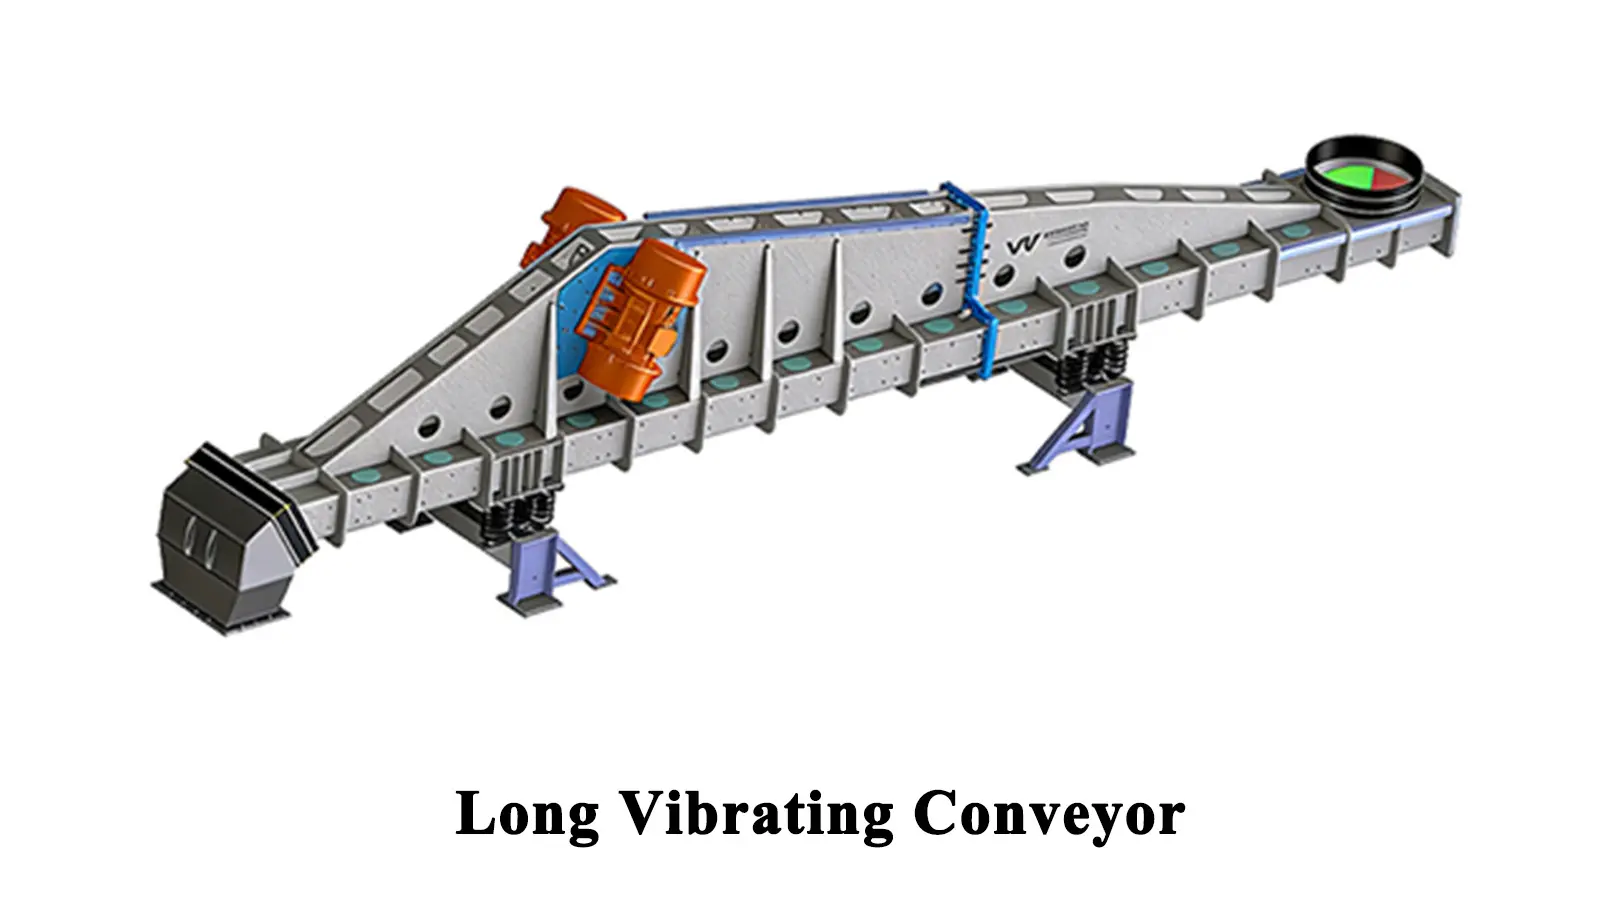
long vibrating conveyor for long-distance bulk material conveying

Long Vibrating Conveyor for Long-Distance Bulk Material Conveying

Features

1. Suitable for long-distance horizontal and slightly inclined material conveying.

2. Ensures stable and uniform material flow with low operation noise.

3. Fully enclosed structure avoids dust spillage and material contamination.

4. Applicable to various powder, granular and bulk materials in multiple industries.

5. Customizable lengths, sizes and materials for different working conditions.


7. Bidirectional Vibrating Conveyor

Two-way Vibrating Conveyor is a high-efficiency directional feeding equipment designed with two discharge outlets. It can flexibly switch between two different conveying directions according to actual production needs, while only conveying materials to one direction at a time. Driven by electromagnetic or vibration motors, it ensures stable, uniform and adjustable material flow, effectively coordinating material supply between different production links or processing equipment. With a compact and reasonable structure, it is widely used in mining, metallurgy, building materials, chemical industry, grain and other bulk material handling systems.
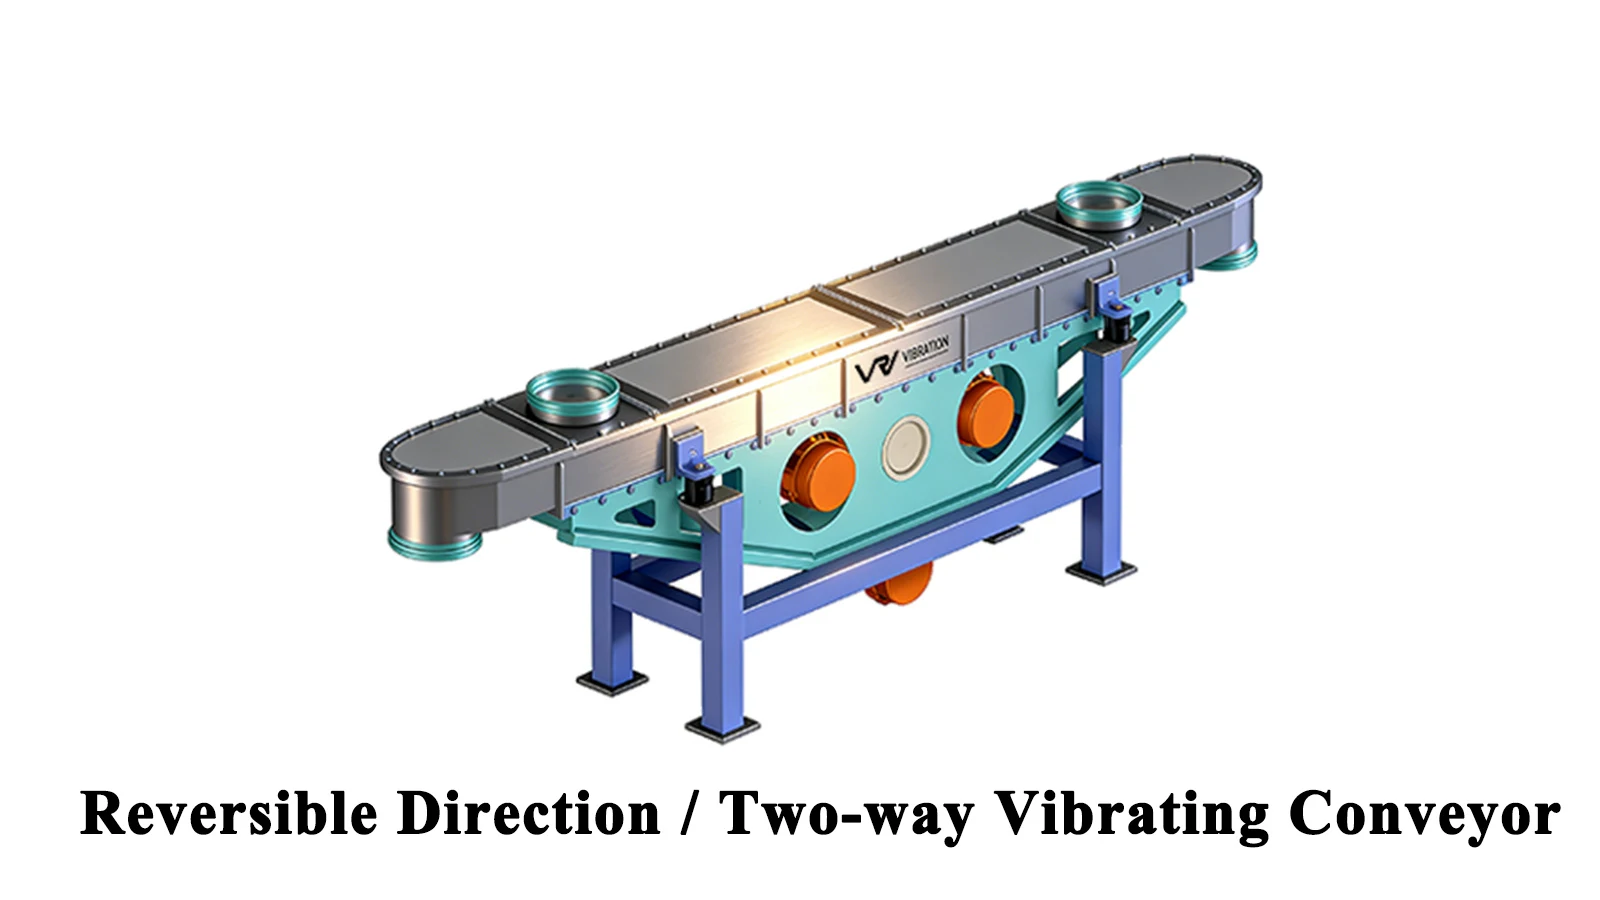
two-way vibrating feeder with dual discharge outlets for directional material feeding

Two-way Vibrating Feeder with Dual Discharge Outlets for Directional Material Feeding

Features

1. Equipped with two discharge outlets and supports flexible direction switching.

2. Conveys materials to only one direction at a time for stable and accurate feeding.

3. Provides uniform and adjustable material flow with reliable and smooth operation.

4. Compact structure saves layout space and optimizes production system configuration.

5. Suitable for powder, granular and block bulk materials in various industrial fields.


If you want to know more about Vibrating Feeder, please click here to download VRV product catalog.
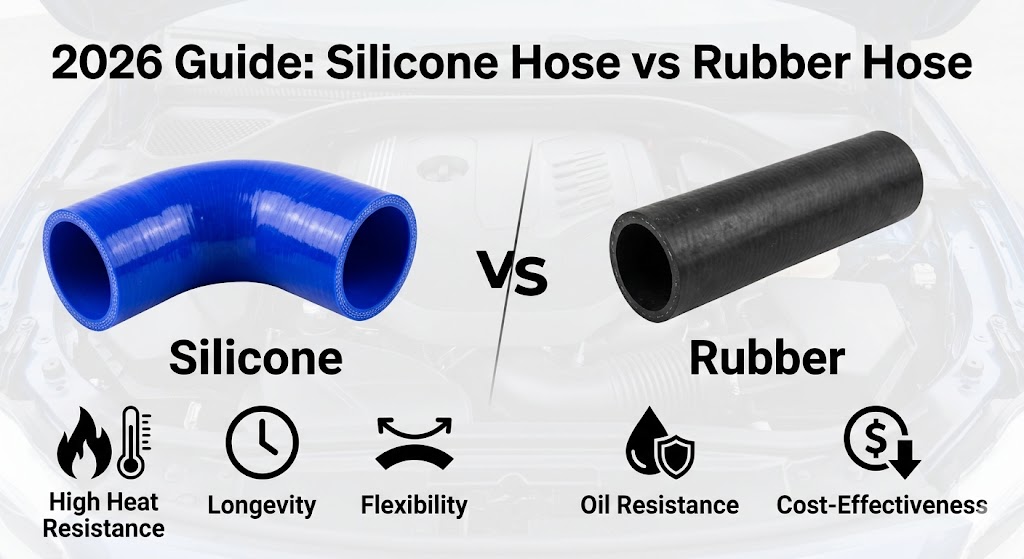
2026 Guide to Automotive Silicone Hose vs Rubber Hose

Quick Comparison: Silicone vs Rubber Hoses

Silicone vs Rubber Hoses


Durability

You want a hose that lasts. Silicone hoses, especially those from Rainbow, deliver exceptional durability. They resist cracking, hardening, and environmental damage. Rubber hoses wear out faster and often require replacement within five years. Rainbow silicone hoses maintain their integrity for over a decade, making them a smart investment.


Temperature and Oil Resistance

Silicone hoses handle extreme temperatures and oil exposure with ease. Rainbow’s silicone hoses withstand up to 180°C and down to -60°C. Rubber hoses struggle above 120°C and degrade when exposed to oil. You gain peace of mind with Rainbow, knowing your hoses perform reliably in harsh conditions.


Flexibility

Silicone hoses offer superior flexibility. You can bend and route Rainbow silicone hoses without kinking or collapsing. Rubber hoses provide moderate flexibility but lose shape over time. This flexibility makes installation easier and ensures consistent performance.


Cost

Rubber hoses cost less upfront. Silicone hoses, including Rainbow, require a higher initial investment. You save money in the long run because Rainbow hoses last longer and reduce replacement frequency.

Maintenance

You spend less time maintaining silicone hoses. Rainbow hoses resist aging, UV damage, and chemical breakdown. Rubber hoses need frequent inspections and replacements. Choosing Rainbow means fewer maintenance headaches and more time enjoying your vehicle.


Pros and Cons: Silicone vs Rubber Hoses

Silicone Hose Advantages

You gain significant benefits when you choose silicone hoses for your vehicle. Silicone hoses deliver improved performance in demanding environments. You experience enhanced durability, which means a reduced need for replacements over the life of your vehicle. Rainbow automotive silicone hoses set the standard for reliability and temperature resistance, making them ideal for performance enthusiasts. You notice that silicone hoses maintain flexibility and strength even after years of use. Their resistance to cracking, swelling, and chemical exposure ensures consistent performance. You also benefit from the vibrant color options that help with quick inspections and custom builds.

Tip: Rainbow silicone hoses offer unmatched performance for both daily drivers and high-performance vehicles.


Silicone Hose Disadvantages

You should consider the higher upfront cost of silicone hoses. Silicone hoses may not always fit perfectly in every application, especially if your vehicle uses custom or rare fittings. Some silicone hoses can absorb certain oils over time, which may affect performance in specific systems. You might also find that silicone hoses require special clamps to prevent leaks. For some vehicle owners, the initial investment in silicone hoses may seem steep, but the long-term benefits often outweigh the drawbacks.


Rubber Hose Advantages

You benefit from the lower initial cost of rubber hoses. Rubber hoses are widely available and easy to replace. Many vehicle owners appreciate the straightforward installation process. Rubber hoses work well for standard applications where extreme performance is not required. You can rely on rubber hoses for basic repairs and short-term solutions.


Rubber Hose Disadvantages

You face limited performance and a shorter lifespan with rubber hoses. Rubber hoses degrade quickly under high temperatures and exposure to engine fluids. You may encounter frequent replacements, which increases maintenance costs. Rubber hoses lack the flexibility and reliability of silicone hoses, especially in performance or high-stress environments. For performance enthusiasts, rubber hoses rarely deliver the improved performance or durability needed for demanding applications.


You get the best results with Rainbow silicone hoses.

  • You enjoy superior durability, temperature resistance, and long-term value.

  • You reduce maintenance and replacement costs.

    For most drivers, Rainbow silicone hoses outperform rubber. Choose rubber only if you need a quick, low-cost fix.


FAQ

How do Rainbow silicone hoses compare to rubber hoses for daily driving?

You get longer lifespan and fewer maintenance issues with Rainbow silicone hoses. Rubber hoses require frequent checks and replacements.


Can you use Rainbow silicone hoses in high-performance engines?

Rainbow silicone hoses handle extreme heat and pressure. You gain reliable performance for turbocharged and racing applications.


Are Rainbow silicone hoses worth the higher upfront cost?

Hose Type

Upfront Cost

Long-Term Value

Rainbow Silicone

Higher

Excellent

Rubber

Lower

Moderate

You save money over time with Rainbow silicone hoses due to fewer replacements.

Fuel Cell Silicone Hose Pros and Cons Explained Simply

Fuel Cell Silicone Hose Pros and Cons Explained Simply

I often get asked if a Fuel Cell Silicone Hose is a smart investment. I appreciate its heat resistance, flexibility, and durability. However, I know fuel permeability and cost can be drawbacks. I trust Rainbow for reliable quality, but I always consider my specific application before deciding.


Key Takeaways

  • Fuel Cell Silicone Hoses offer excellent heat resistance, making them ideal for environments with extreme temperature changes. This prevents unexpected failures in fuel cell systems.

  • Flexibility is a key advantage of silicone hoses. They bend easily, allowing for easier installation in tight spaces without kinking or collapsing.

  • While silicone hoses are durable, they can be more expensive than standard hoses. Always consider your budget and the specific needs of your application before making a choice.


Fuel Cell Silicone Hose Benefits

Fuel Cell Silicone Hose Benefits


Heat Resistance

I have seen how a Fuel Cell Silicone Hose stands up to extreme temperatures. When I work with fuel cell systems, I notice that heat can quickly damage standard rubber hoses. Silicone hoses, on the other hand, handle both high and low temperatures without losing their shape or strength. I often recommend them because they can withstand repeated heating and cooling cycles. This makes them ideal for environments where temperature changes happen often. I trust Rainbow hoses for their consistent performance in these demanding conditions.

Tip: If your fuel cell setup faces frequent temperature swings, silicone hoses can help prevent unexpected failures.


Flexibility

I value flexibility when I install hoses in tight engine bays or compact fuel cell systems. A Fuel Cell Silicone Hose bends easily without kinking or collapsing. This flexibility allows me to route hoses around obstacles and fit them into small spaces. I find installation much easier compared to rigid or stiff alternatives. Rainbow hoses, in particular, offer a smooth and pliable feel that speeds up my work and reduces frustration.

  • Easy to route in confined spaces

  • Maintains shape even when bent

  • Reduces installation time


Durability

Durability matters to me because I want components that last. I have used Fuel Cell Silicone Hoses that remain reliable after years of service. Silicone resists cracking, splitting, and hardening, even when exposed to harsh chemicals or UV light. I notice that Rainbow hoses keep their integrity longer than many generic brands. This durability means fewer replacements and less downtime for maintenance.


Impact Protection

I have seen hoses get bumped or knocked during routine checks or repairs. A Fuel Cell Silicone Hose absorbs impacts better than many other materials. The thick silicone walls cushion against accidental hits, which helps prevent leaks or ruptures. I appreciate this extra layer of protection, especially in busy workshops or mobile applications.

Note: While no hose is indestructible, silicone offers a good balance between flexibility and impact resistance.

I rely on Rainbow for hoses that combine all these benefits. Their products help me build safer and more reliable fuel cell systems.


Fuel Cell Silicone Hose Drawbacks

Fuel Permeability

I have noticed that a Fuel Cell Silicone Hose sometimes allows fuel molecules to seep through its walls. This permeability can lead to vapor loss or even fuel odors in the workspace. When I work with sensitive fuel cell systems, I pay close attention to this issue. Some fuels, especially those with aggressive chemicals, can pass through silicone more easily than through other materials. I always check the specifications and test the hose before installation. If I need to minimize fuel loss, I consider using a liner or selecting a hose with lower permeability.

Note: Careful selection is essential. Not every silicone hose suits every fuel type.


Brittleness Over Time

I have seen silicone hoses become brittle after years of exposure to heat, chemicals, and UV light. This brittleness can cause cracks or leaks, especially in older fuel cell systems. I inspect hoses regularly and replace them when I see signs of hardening or surface damage. Although silicone resists many environmental factors, it does not last forever. I recommend storing spare hoses away from direct sunlight and extreme temperatures to extend their lifespan.

  • Inspect hoses for stiffness or cracks

  • Replace hoses showing signs of brittleness

  • Store hoses in cool, dry places


Compatibility Issues

I always check compatibility before installing a Fuel Cell Silicone Hose. Some fuels and additives react with silicone, causing swelling, degradation, or leaks. I consult manufacturer charts and test samples when I work with new fuel blends. Compatibility issues can lead to system failures or safety hazards. I never assume that a silicone hose will work with every fuel. I rely on trusted brands and clear documentation to guide my choices.

Fuel Type

Silicone Hose Compatibility

Gasoline

Limited

Ethanol

Limited

Diesel

Moderate

Hydrogen

Good

Methanol

Limited

Tip: Always verify compatibility with your specific fuel before installation.


Cost

I have found that Fuel Cell Silicone Hose costs more than standard rubber or plastic hoses. The higher price reflects its advanced properties, but it can strain a project budget. I weigh the benefits against the expense when I plan a fuel cell system. Sometimes, I choose silicone for critical areas and use less expensive materials elsewhere. Mechanical strength can also be a concern. Silicone hoses may not handle high-pressure applications as well as reinforced alternatives. I balance cost, performance, and safety for each project.

  • Higher upfront cost

  • May require reinforcement for high-pressure use

  • Consider budget and application needs

Alert: Evaluate both cost and mechanical strength before making a final decision.

Choosing the Right Hose for Fuel Cells

Choosing the Right Hose for Fuel Cells

Application Needs

I always start by looking at the specific requirements of my project. I ask myself what type of fuel the system uses, what temperature range the hose must handle, and how much pressure it will face. I consider the space available for installation and whether the hose needs to bend around tight corners. When I choose a Fuel Cell Silicone Hose, I check if it matches the chemical compatibility and mechanical strength needed for the application. I never skip this step because the wrong hose can lead to leaks or system failures.

Tip: Write down your system’s fuel type, temperature range, and pressure before shopping for hoses.


Alternatives

I know that silicone is not the only option. Sometimes, I use fluorocarbon, PTFE, or reinforced rubber hoses. Each material has its own strengths and weaknesses. For example, PTFE hoses resist fuel permeability better than silicone, but they can be less flexible. Reinforced rubber works well for high-pressure systems, but it may not last as long in extreme heat. I compare these alternatives based on cost, durability, and compatibility with the fuel.

Hose Material

Flexibility

Heat Resistance

Fuel Permeability

Cost

Silicone

High

High

Moderate

Higher

PTFE

Moderate

High

Low

High

Reinforced Rubber

Moderate

Moderate

Low

Lower


Maintenance Tips

I make regular inspection a habit. I check hoses for cracks, stiffness, or discoloration every few months. I replace any hose that shows signs of wear. I also keep hoses clean and free from oil or debris. Proper storage extends hose life, so I store spares in a cool, dry place away from sunlight. These steps help me avoid unexpected failures and keep my fuel cell system running safely.

Alert: Regular maintenance prevents costly breakdowns and extends the life of your hoses.


I see clear benefits in using Fuel Cell Silicone Hoses: heat resistance, flexibility, and durability. Drawbacks include fuel permeability and higher cost. I choose Rainbow hoses for reliable performance. For most fuel cell projects, I recommend Rainbow silicone hoses if you need quality and long-term value.


FAQ

What makes Rainbow silicone hoses different from other brands?

I trust Rainbow hoses for their consistent quality. I notice they last longer and resist heat better than many generic options.

Can I use a silicone hose for all fuel types?

I always check compatibility charts. Some fuels, like gasoline or ethanol, can damage silicone. I recommend testing before installation.

How often should I replace my fuel cell silicone hose?

I inspect hoses every few months. If I see cracks, stiffness, or leaks, I replace them right away to avoid system failures.

Rainbow Manufacturing – Your Reliable Silicone Hose Partner

Rainbow Manufacturing is an IATF 16949 and ISO 9001 certified silicone hose manufacturer with over 15 years of experience in performance silicone hoses and molded components. We supply a wide range of products including silicone tubing, fuel cell hoses, and custom-molded parts for automotive, railway, healthcare, electronics, and agricultural machinery. Our commitment to quality and precision has made us a trusted name in the industry.

All our FDA-grade silicone hoses and braided versions are fully compliant with RoHS, REACH, LFGB, FDA 21 CFR 177.2600, and EC 1935/2004 standards. They are BPA-free, non-toxic, and safe for food contact applications. Additionally, our vehicle hoses — such as turbocharger, air intake, CAC, heater, and vacuum hoses — meet SAE J20, J30, and J2006 specifications, while our fire-rated options comply with EN45545 and UL94-V0 for railway use.

We also manufacture fuel cell silicone hoses and FKM-lined versions for fuel cell power systems, meeting FDA, REACH, and RoHS requirements. Whether you need fuel-resistant, high-temperature, wire-reinforced, or complex-shaped hoses, Rainbow Manufacturing welcomes custom silicone hose designs for any challenge. Visit www.rainbow-manufacturing.com to learn more or request a quote today.

Silicone Radiator Hose Secrets for Hot Motorcycles

You ride your motorcycle in tough conditions. Heat builds up fast, and you need parts that stand up to the challenge. A silicone radiator hose gives you strong heat resistance, lasting durability, and reliable performance. You can choose custom colors and shapes to match your bike and show your style. The right hose helps your engine stay cool and keeps your ride looking sharp.

Key Takeaways

  • Silicone radiator hoses withstand extreme temperatures up to 356°F, ensuring your engine stays cool even in tough conditions.
  • These hoses last significantly longer than rubber hoses, with a lifespan of 5 to 15 years, saving you money on replacements.
  • Custom-fit silicone hoses improve cooling efficiency and prevent leaks, enhancing your motorcycle's performance and reliability.
  • Regular maintenance, including inspections every few months, helps extend the life of your silicone hoses and keeps your cooling system in top shape.
  • Investing in high-quality silicone hoses from trusted brands ensures durability and performance, giving you peace of mind on every ride.

Silicone Radiator Hose Features

High Temperature Resistance

You need a radiator hose that can handle extreme heat. Silicone radiator hose stands out because it resists temperatures much higher than standard rubber hoses. You can see the difference in the table below:


Hose Material Max Temperature Best For Common Uses
Silicone 180°C (356°F) Extreme heat, performance, longevity Turbo/intercooler, coolant, heater, industrial steam
EPDM Rubber 120°C (248°F) Most automotive cooling/heating needs Radiator, heater, coolant hoses


Laboratory tests show that silicone radiator hose can withstand temperatures up to 356°F for long periods. You do not have to worry about softening or bursting. The hose keeps its shape and strength under pressures up to 174 PSI. After 1,000 hours of testing with coolant at high pressure, the hose showed no leaks or cracks. You can trust it to protect your engine from overheating.

RAINBOW’s hoses meet strict quality standards. The company holds ISO 9001 certification and complies with SAE J20 R4 Class A specifications. You get a product that passes tough industry tests.

Flexibility & Durability

You want a hose that bends easily and lasts for years. Silicone radiator hose uses 3-ply or 4-ply polyester reinforcement. This design gives you flexibility without kinking or splitting. Flexibility tests prove that the hose can bend over 100 times and still work perfectly.

You can expect a long lifespan. Most silicone radiator hoses last between 5 to 8 years under continuous high-temperature conditions. High-quality hoses, like those from RAINBOW, may last even longer. You save money and avoid frequent replacements.

RAINBOW offers custom fit options. You can choose hoses that match your motorcycle’s unique shape and size. You also get vibrant color choices, such as black, red, or blue. Your bike looks great and performs even better.

Chemical Compatibility

You need a hose that resists chemicals found in motorcycle cooling systems. Silicone radiator hose handles water, air, coolant, and small amounts of oil mist. Premium materials make the hose resistant to heat, pressure, and chemicals. These features help the hose deliver reliable performance.

You do not have to worry about leaks or damage from common fluids. The hose stays strong and keeps your engine safe. RAINBOW’s hoses are not recommended for oil, fuel, or power steering fluid, but they work perfectly for cooling applications.

Benefits for Hot Motorcycles

Preventing Overheating

You want your motorcycle to stay cool, even when you push it hard. A silicone radiator hose helps your engine avoid overheating in extreme conditions. The special silicone material keeps its shape and strength from -60°C to +230°C. It does not deform, even when your cooling system faces high pressure. This means your coolant flows smoothly, and your engine stays at the right temperature.

Here is a table that shows how silicone hoses protect your engine:

Feature Description
Extreme Temperature Performance Specially formulated silicone withstands continuous temperatures from -60°C to +230°C. Maintains flexibility and integrity in extreme riding conditions. Prevents hose deformation under high-pressure cooling systems.
Cooling System Advantages Superior heat dissipation properties. Reduced risk of coolant boiling and vapor lock. Maintains optimal engine temperature under heavy load. Prevents coolant loss and overheating issues.
Durability & Maintenance 5x longer service life compared to OEM rubber hoses. Resists ozone cracking and UV degradation. No more periodic hose replacements. Easy to clean and maintain.


Field tests prove the value of silicone hoses. For example, a 1968 Mustang GT/CS used silicone hoses during racing. The car kept its coolant and held safe temperatures for four hours, even with pressure spikes. Diesel generators with silicone hoses survived continuous exposure to 320°C and short bursts up to 350°C. The hoses did not swell or leak.

Longevity Under Stress

You need parts that last. Silicone radiator hoses resist cracking, swelling, and hardening, even after years of use. They do not break down from ozone, UV light, or chemicals. Riders who switch to silicone hoses often find that these hoses outlast the bike itself. One rider reported that after five years of heavy use, his hoses showed no cracks. In contrast, rubber hoses on his old bike failed every two years.

  • Silicone hoses resist thermal degradation and stay flexible over time.
  • They last much longer than rubber hoses, which often crack or harden.
  • Silicone hoses keep their shape and strength, even in high heat or under heavy engine stress.
  • You do not need to replace them as often, which saves you time and money.

In tough tests, silicone hoses handled temperatures from -65°F to 500°F. Rubber hoses softened and cracked, but silicone hoses stayed strong. They passed pressure tests up to 20 bar without bursting. This means you can trust your cooling system, even on long rides or in extreme heat.

Performance Boost

You want your motorcycle to run at its best. Silicone radiator hoses improve coolant flow and help your engine perform better. Their smooth inner surface reduces friction, so coolant moves quickly and evenly. This keeps your engine at the right temperature and protects it from damage.

  • Silicone hoses are flexible and durable, which helps your cooling system work efficiently.
  • They resist high temperatures, so they do not swell or block coolant flow.
  • Premium silicone hoses keep your engine safe by preventing leaks and maintaining steady coolant movement.

When you use a silicone radiator hose, you get better cooling, fewer breakdowns, and more reliable performance. Your engine stays cool, even when you ride hard or in hot weather. You spend less time on repairs and more time enjoying your motorcycle.

Silicone Radiator Hose vs. Other Materials

Silicone vs. Rubber

You want your motorcycle to perform well in every condition. Choosing the right hose makes a big difference. Silicone radiator hose stands out when compared to traditional rubber hoses. Look at the table below to see how these materials differ:

Property Silicone Hose EPDM Rubber Hose
Max Continuous Temp 350°F (177°C) 257°F (125°C)
Min Temperature -65°F (-54°C) -40°F (-40°C)
Typical Service Life 8–15+ years 3–7 years
UV / Ozone Resistance Excellent Moderate
Pressure Resistance High Moderate
Oil / Fuel Resistance Poor Good
Flexibility at Low Temp Remains flexible Stiffens / can crack
Typical Price (per foot) $5–$20 $1–$6
Color Options Wide Mostly black


You see that silicone hoses handle higher temperatures and last longer. They resist UV and ozone damage, so you do not need to worry about cracks or fading. Rubber hoses cost less at first, but you replace them more often. Over five years, silicone hoses save you money because you avoid frequent replacements and emergency repairs.

  • Silicone hoses last 10–15 years.
  • Rubber hoses need replacement every 3–5 years.
  • Fewer replacements mean lower maintenance costs.
  • You spend less on materials and labor.
  • Silicone vs. Reinforced Hoses

    You may wonder how silicone hoses compare to reinforced hoses made from EPDM rubber. Silicone hoses offer several advantages:

    • They withstand temperatures from -50°C to +220°C, while EPDM hoses only handle -40°C to +125°C.
    • Silicone resists wear, oil, grease, and chemicals better than EPDM.
    • You get excellent resistance to weather and UV light, so your hose stays strong in harsh environments.
    • Silicone hoses remain flexible and do not kink or collapse, even when your motorcycle vibrates or moves.

    You choose silicone hoses for durability and performance. They keep your cooling system reliable and efficient, even during tough rides. If you want a hose that lasts and looks great, silicone is the best choice.

    Choosing Silicone Radiator Hose

    Construction Quality

    You want a hose that lasts and performs well. Construction quality matters most. Look for hoses with strong reinforcement. Most high-quality hoses use 3-ply or 4-ply layers. These layers help the hose stay flexible and strong under pressure. Polyester is the most common reinforcement. Some hoses use fiberglass or meta-aramid for special needs.

    Fabric Reinforcement Characteristics
    Polyester Most common and affordable
    Fiberglass Higher temperature resistance
    Nomex® Specialized applications
    Meta-Aramid High-performance applications


    You should check for ISO 9001 certification and SAE J20 Class A compliance. These standards show that the hose meets strict quality and safety rules. Hoses with these certifications give you peace of mind.

    • 3-ply and 4-ply hoses are common.
    • Both types meet SAE J20 standards.
    • Extra plies may be needed for special uses.

      Fit & Compatibility

      You need a hose that fits your motorcycle perfectly. A good fit keeps your cooling system working well. Custom options help you match the hose to your bike’s shape and size. RAINBOW offers custom solutions. You can send your drawings or samples. Their team will make hoses that fit your exact needs.

      • Custom hoses improve cooling efficiency.
      • You can choose colors to match your bike.
      • A perfect fit prevents leaks and overheating.

        Brand Reputation

        You want to buy from a trusted brand. Brands like Samco Sport and Mishimoto have strong reputations for quality. RAINBOW stands out with ISO 9001 certification and custom solutions. You can trust these brands to deliver reliable hoses for your motorcycle.

        • Samco Sport is known for racing and performance.
        • Mishimoto specializes in cooling systems.
        • RAINBOW offers certified, custom-fit hoses.
  • Installation & Maintenance

    Installation Steps

    Installing a silicone radiator hose on your motorcycle helps you get the best cooling performance. You can follow these steps to make sure you do it right:

    1. Drain the Coolant: Place a drain pan under the radiator. Open the drain valve and let the coolant flow out. Remove the old hose completely. Check that no rubber pieces stay in the radiator necks.
    2. Inspect the Radiator Necks: Clean the surfaces where the hose connects. Use a clean rag to wipe away dirt or debris. A clean surface prevents leaks.
    3. Position the Silicone Hose: Slide the new silicone hose onto the radiator neck. Make sure the hose sits evenly and does not twist.
    4. Install the Clamps: Put stainless steel clamps over the hose ends. Do not tighten them yet.
    5. Connect the Cylinder Side: Move the hose to the cylinder head port. Gently wiggle the hose if needed to line up the ports.
    6. Final Clamp Tightening: Once both ends fit well, tighten the clamps. Use a torque wrench if you have one. Aim for 5-7 Nm. The hose should feel snug, not crushed.
    7. Refill and Bleed: Pour in fresh coolant. Start the engine and let it warm up. Check for leaks while the engine runs.
  • Maintenance Tips

    You want your silicone radiator hoses to last as long as possible. Regular checks help you spot problems early and keep your cooling system working well.

    • Inspect your hoses every few months for signs of wear, swelling, or cracks.
    • Replace silicone coolant hoses every 4 to 6 years, even if they look fine. High heat and pressure can weaken hoses over time.
    • Clean the hose surfaces with a damp cloth to remove dirt and oil.
    • Check clamps for tightness. Loose clamps can cause leaks.
    • Watch for coolant leaks around hose connections after long rides.

You want your motorcycle to stay cool and look great. Silicone radiator hoses give you strong heat resistance, long-lasting durability, and better performance. When you choose certified, custom-fit hoses like those from RAINBOW, you get:

  • Heat-resistant fibers that handle high temperatures and pressure
  • High-strength silicone that lasts longer than rubber hoses
  • Direct-fit designs for better fitment and style

Upgrade your cooling system for more reliability and a bold look on every ride.

FAQ

What makes silicone radiator hoses better than rubber hoses?

You get higher heat resistance and longer lifespan with silicone hoses. They resist cracking and fading from sunlight. Silicone hoses also come in many colors, so you can match your bike’s style.

Can I use silicone radiator hoses for all motorcycle fluids?

You should use silicone hoses for coolant, water, and air. They handle small amounts of oil mist. Do not use them for fuel, oil, or power steering fluid.

How do I know if a silicone hose fits my motorcycle?

Check your motorcycle’s model and measurements. Custom-fit options from brands like RAINBOW let you send drawings or samples. You get a hose that matches your bike perfectly.

How often should I replace silicone radiator hoses?

Inspect your hoses every few months. Replace them every 4 to 6 years, even if they look good. High heat and pressure can weaken hoses over time.

Do silicone radiator hoses improve engine performance?

You get smoother coolant flow and better heat management. This helps your engine stay cool and run more efficiently. Silicone hoses also reduce the risk of overheating.

If you want to get more details about us, plz click www.rainbow-manufacturing.com.

The Advantages of Custom Silicone Coolant Hoses

Need a hose that fits tight bends, handles vacuum pressure, and withstands tough working conditions? Custom silicone coolant hoses are the answer. They perform reliably in environments involving water-air coolant, boost pressure, and light oil mist, making them ideal for automotive engine compartments, large diesel trucks, off-road heavy equipment, and power generators. Plus, they meet the requirements of SAE J20 R4 specification.

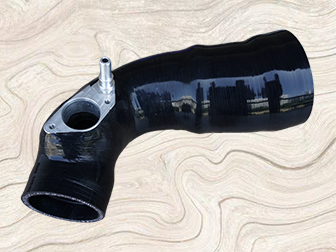
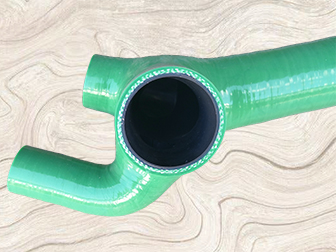
What makes silicone the superior choice? Unlike traditional rubber coolant hoses, silicone coolant hose offers a much higher temperature rating, operating smoothly from -55°C up to 200°C. It retains flexibility over time and resists cracking, ozone attack, sunlight, and many chemicals. To add extra strength, these hoses are often built with 3-ply or 4-ply polyester reinforcement, with wall thickness options of 4.5mm and 5.0mm.

Best of all, every aspect of the silicone coolant hose can be tailored to your needs—diameter, shape, length, and color are all customizable. Whether you have a simple sketch or a physical sample, simply send it to us and we will create a custom coolant hose that fits your application perfectly. High-temperature rated options are also available upon request.

Maximizing Machine Uptime Preventative Maintenance for Heavy-Duty Balers and Shears

To maximize the lifespan and ROI of heavy-duty metal recycling machinery, facilities must implement a strict preventative maintenance schedule focusing on hydraulic fluid purity, daily cylinder seal inspections, and regular replacement of wear plates. Consistent maintenance prevents catastrophic hydraulic failures, reduces unplanned downtime, and ensures continuous high-volume throughput.

The True Cost of Unplanned Downtime In the highly competitive metal recycling industry, equipment downtime is the silent killer of profitability. When a heavy-duty processing machine suddenly breaks down, the financial impact extends far beyond the cost of replacement parts. It causes massive bottlenecks in the yard, delays outbound shipping contracts, and leaves expensive labor forces standing idle. For procurement managers and facility operators, protecting your capital investment means shifting from a reactive "fix-it-when-it-breaks" mentality to a proactive preventative maintenance strategy.

Protecting the Hydraulic Lifeblood The core of any modern compaction or cutting machinery is its hydraulic system. Whether you are operating a heavy-duty scrap metal baler or a massive gantry shear, hydraulic fluid acts as the lifeblood of the machine. The most common cause of catastrophic failure is fluid contamination.

Microscopic metal shavings, dust, and water condensation can bypass worn seals and enter the hydraulic reservoir. Over time, these contaminants act like liquid sandpaper, destroying expensive pumps and scoring hydraulic cylinders from the inside out. To prevent this, operators must strictly adhere to OEM guidelines regarding oil filter replacements and fluid sampling. Additionally, monitoring the hydraulic oil temperature is critical; running a machine with overheated oil rapidly degrades the fluid's viscosity and destroys internal O-rings.

Inspecting Structural Integrity and Wear Parts Heavy machinery is subjected to immense, repetitive stress. Daily visual inspections are critical for catching small issues before they escalate. Operators should regularly check the structural integrity of the press chamber for micro-fractures along the weld lines.

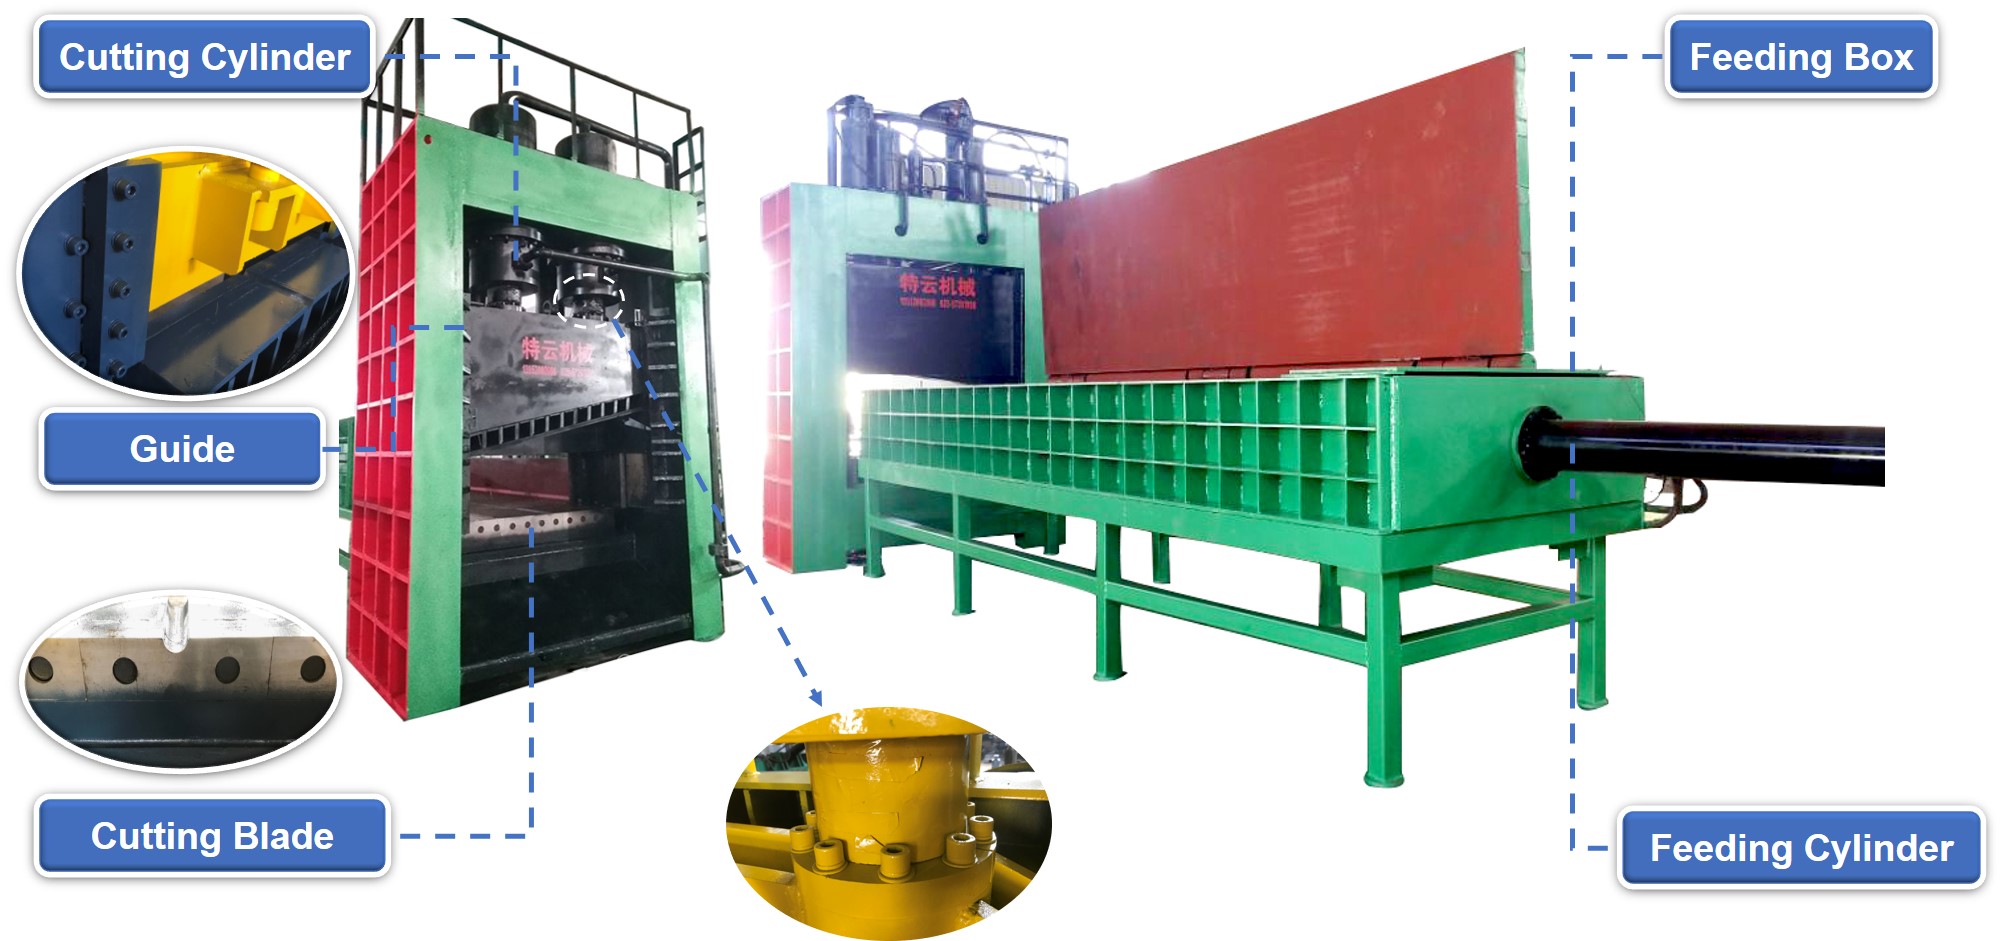
Furthermore, wear parts such as inner liner plates and cutting blades must be monitored. If you are utilizing an industrial scrap metal shear, operating with dulled blades forces the hydraulic system to work significantly harder to achieve the same cut. This spikes electrical energy consumption and places unnecessary strain on the motors. Regularly rotating or replacing hardened alloy blades ensures clean, efficient cuts and protects the machine's primary drive systems.

Partnering for Long-Term Success Ultimately, the longevity of your recycling equipment depends on a combination of rigorous daily maintenance and rapid access to high-quality spare parts. When sourcing machinery, partnering with a manufacturer that provides comprehensive maintenance training, intuitive PLC diagnostic systems, and a reliable global supply chain for replacement parts is essential for keeping your yard running at peak capacity year after year.

Choosing a Professional Scrap Metal Shear Manufacturer Engineering for Performance

Selecting a professional scrap metal shear manufacturer requires a deep evaluation of hydraulic stability, blade alloy quality, and the machine's ability to process diverse metal grades. Leading manufacturers now offer specialized alligator shears for agile, manual cutting of non-ferrous materials and heavy-duty gantry shears for automated, high-volume processing of structural steel and heavy iron.

The Strategic Importance of Precision Shearing

In the global metal recycling landscape, the "first cut" is often the most critical. Processing bulky, oversized scrap into furnace-ready dimensions is a prerequisite for high-value sales to smelters. For scrap yard operators, the challenge lies in finding a manufacturer that balances raw cutting force with operational reliability. Whether you are dealing with thin-walled aluminum profiles or massive I-beams, the quality of your scrap metal shear dictates your daily tonnage and the overall wear and tear on your processing line.

Material Versatility: From Alligators to Gantry Powerhouses

A professional manufacturer must provide a diverse portfolio of machinery to match the varied scrap mix of modern industrial zones. For non-ferrous specialists processing copper cables, aluminum extrusions, and smaller steel pipes, a high-speed alligator shear machine is the gold standard. These units are prized for their hinged-jaw agility and lower energy consumption, making them perfect for manual sorting and rapid-fire cutting tasks.


However, as the industry moves toward processing heavier structural steel and demolition scrap, the demand for brute hydraulic power increases. This is where heavy-duty gantry shears and container shears excel. These machines utilize advanced PLC systems to automate the feeding and shearing process, allowing for continuous operation that drastically reduces labor costs. By investing in a high-quality hydraulic scrap metal shear, facilities can transition from manual, low-volume processing to industrial-scale throughput.

Engineering Excellence: The Teyun Advantage

What distinguishes a top-tier manufacturer is the engineering behind the hydraulic system and the metallurgical quality of the blades. Modern shearing equipment must withstand extreme friction and repetitive stress. Teyun’s machinery utilizes hardened alloy steel blades that maintain their edge significantly longer than standard carbon steel alternatives, reducing maintenance downtime. Furthermore, our hydraulic architectures are designed with integrated cooling systems, ensuring that even in high-temperature environments—common in the Middle East and Southeast Asia—the machine maintains stable pressure without overheating.

Final Thoughts for Global Buyers

Upgrading your shearing infrastructure is a decade-long investment. When choosing a manufacturer, prioritize those who offer comprehensive turnkey solutions, from installation support to rapid spare parts availability. A robust shearing line not only prepares your scrap for the highest market value but also eliminates the operational bottlenecks that hinder growth in a competitive recycling market.

How to Choose the Right Diamond Grinding Segments for Your Concrete Grinder A 7-Point Procurement Checklist

A concrete grinder is only as effective as the diamond tooling mounted on it. Many contractors lose hours — and thousands of dollars — not because their grinder is underpowered, but because their diamond grinding segment is mismatched to the concrete they're working on.


1. Test Concrete Hardness First

The single most important variable in diamond tooling selection is the hardness of the concrete. Getting this wrong leads to glazed-over segments or rapid segment loss.

Hard concrete (6–7 Mohs) → Soft bond
Soft concrete (3–5 Mohs) → Hard bond


2. Match Grit Size to the Task

Grit size determines whether a segment removes material aggressively or refines a surface smoothly. Never skip grit stages to save time.

16–40 Grit: Coating removal, heavy leveling
70–120 Grit: First grinding pass
200–400 Grit: Honing, matte finish
800–3000+ Grit: Polishing, high gloss


3. Understand Segment Geometry
The shape of a diamond grinding segment is not cosmetic; it influences cutting speed and dust evacuation.

Arrow / "S"-shape: Higher point pressure for aggressive cutting

PCD (Polycrystalline Diamond): Best for scraping thick coatings like epoxy or mastic


4. Wet vs. Dry Grinding

Wet grinding extends tool life by 2–3x but requires slurry management. Dry grinding is more convenient but requires integrated HEPA vacuum systems for OSHA compliance.


5. Consider Grinder Type and Pressure

Planetary grinders are forgiving on segments, while rotary (single-disc) grinders apply concentrated force. Match your segment structural integrity to your machine type.


6. Calculate Cost Per Square Foot

Grinding is just the beginning. A complete project requires a sequence: PCD → Metal-bond Segments → Densifiers → Resin Polishing Pads.


7. The Full Surface Prep System

Grinding is just the beginning. A complete project requires a sequence: PCD → Metal-bond Segments → Densifiers → Resin Polishing Pads.


Our Manufacturing Advantages in Floor Grinding Segments

In the demanding world of surface preparation, SANG stands out as a specialized manufacturer of high-performance floor grinding segments. Our advantages are built on 30+ years of empirical data and material science:


Precision Bond Customization

We don't believe in "one size fits all." SANG has developed over 50 unique bond formulas specifically for floor prep, ensuring the perfect match for concrete ranging from 3-Mohs (extra soft) to 8-Mohs (extra hard).

Full-System Compatibility

Our grinding shoes and discs are designed to fit all major floor grinding brands (Husqvarna, HTC, Scanmaskin, Lavina, etc.) with various backing options like Redi-Lock, Magnetic, or Bolt-on systems.


Cost-Efficiency for Large-Scale Projects

By optimizing diamond concentration and bond wear-rates, SANG segments deliver a lower "cost-per-square-foot" compared to industry benchmarks, making them the preferred choice for massive industrial warehouse projects.


Corporate Strength & Global Brand Power

SANG Diamond Tools — A Legacy of Leadership Since 1993


Top 10 Industry Leader

Established in 1993, SANG is recognized as a Top 10 Manufacturer in China's diamond tool industry. With an annual tax contribution reaching millions, we are a fiscally strong and reliable partner you can trust for long-term supply.


Scientific Innovation (PhD R&D Team)

Innovation is in our DNA. Our R&D center is led by multiple PhDs from prestigious universities, focusing on molecular-level bond design. We don't just sell tools; we provide Exclusive Construction Solutions tailored to your specific job site challenges.


Large-Scale Production & Capacity

With a workforce of 100+ dedicated workshop employees, SANG operates high-capacity automated production lines. We guarantee short lead times and the ability to fulfill container-load orders without compromising quality.


Globally Validated Quality

We hold numerous national industry patents and a comprehensive range of international certificates for our diamond saw blades and grinding tools. Our quality is validated by the most stringent markets in North America and Europe.


Professional Multilingual Communication

Communication is the key to successful partnership. Our sales team consists entirely of English Major (TEM-8) graduates. Furthermore, we offer support in various minority languages (including French, Persian, Spanish, etc.), ensuring zero-barrier communication and precise requirement handling.


On-Site & Remote Technical Support

We stand behind our products. Our technical engineers offer both online video consultations and offline on-site support to assist with machine calibration, tooling selection, and troubleshooting at your project site.


When you choose SANG, you are not just buying a grinding segment; you are partnering with a 30-year industry powerhouse dedicated to your project's success.

Contact Our Expert Team Today:

WhatsApp/WeChat: +8613808521603
Email: info@sangtools.com
Website: www.sangtools.com


FAQ

Q: What is a diamond grinding segment and how does it work?
A: It is a metal-bond abrasive block with synthetic diamonds. It abrades concrete by exposing new diamonds as the metal bond wears away.


Q: Can I use the same segments for granite and concrete?
A: No. Granite segments will typically glaze over on concrete. Always use concrete-specific formulas.


The EV Revolution and Metal Recycling How to Equip Your Yard for the New Scrap Mix

The rapid expansion of electric vehicle (EV) manufacturing is transforming the scrap metal industry by introducing massive volumes of lightweight aluminum chips and Advanced High-Strength Steel (AHSS). To maintain profitability, recycling facilities must upgrade to specialized briquetting presses for aluminum recovery and high-force gantry shears capable of cutting modern, ultra-tough vehicle chassis.

The Changing Anatomy of Scrap Metal The traditional scrap metal mix is evolving rapidly. As global automakers transition from internal combustion engines to electric vehicles (EVs), the materials entering recycling yards and processing facilities are shifting dramatically. Heavy cast iron engine blocks are actively being replaced by lightweight aluminum battery housings, electric motor casings, and complex, high-strength steel structural frames. For scrap yard operators and metal brokers, this new composition presents both a highly lucrative market opportunity and a severe operational challenge. Standard, legacy processing equipment is often highly inefficient—or entirely incapable—of handling these modern, specialized automotive materials.

Maximizing Aluminum Yield in a Lightweight Era The global surge in EV production has led to a massive increase in aluminum CNC machining across the automotive supply chain. This manufacturing process generates hundreds of tons of loose, wet aluminum swarf and turnings. As industry experts know, smelting loose aluminum chips is highly inefficient due to severe surface oxidation, which can result in a devastating 20% to 30% material loss in the furnace.

To capitalize on the high market value of automotive-grade aluminum, recycling facilities must process this specific waste using a high-pressure metal briquetting machine. By compressing the loose, chaotic swarf into ultra-dense, solid cylindrical blocks, facilities prevent metal oxidation during the melting process, effectively maximizing their overall metallurgical yield. Furthermore, the extreme hydraulic pressure extracts valuable cutting fluids, allowing the oils to be recovered and ensuring the briquettes meet the strict, smoke-free environmental standards demanded by modern foundries.

Conquering Advanced High-Strength Steel (AHSS) While EVs utilize significantly more lightweight non-ferrous metals, their core safety frames rely heavily on Advanced High-Strength Steel (AHSS). This specific material is exceptionally tough, highly resistant to deformation, and designed specifically to protect heavy lithium-ion battery packs during severe collisions.

When these modern vehicles or manufacturing offcuts reach the scrap yard, legacy cutting equipment simply lacks the power to process them efficiently, leading to rapidly dulled blades, stalled motors, and costly downtime. Upgrading to a heavy-duty industrial scrap metal shear is no longer an optional upgrade; it is an operational necessity. A modern, robust gantry shear delivers the immense, concentrated hydraulic force required to cleanly slice through AHSS automotive frames without continuous breakdowns, ensuring your yard maintains high-speed, continuous throughput regardless of the vehicle's structural integrity.


Future-Proofing Your Facility
Adapting to the EV revolution is critical for the survival and growth of any modern metal recycling plant. By strategically investing in the right high-pressure and high-force processing equipment today, operators can transform challenging new waste streams into premium, highly profitable commodities.